Why the Fourteenth Printer Did Not Increase Output
A distributor's customer runs eleven enclosed FDM machines and ships roughly 340 parts a week. They bought a twelfth machine expecting throughput to rise by about nine percent. Weekly output moved from 340 to 352 parts. The owner concluded the new machine was defective.
It was not. The line had a printing capacity of around 460 parts a week and a downstream capacity of 355. Every part printed above 355 went into a queue of unfinished work that grew until the finishing bench ran out of space, at which point the floor started prioritising by who shouted loudest. Adding print capacity to a line whose constraint sits downstream does not raise output. It raises work in progress, queue length, and the number of parts sitting exposed on a shelf waiting for their turn at a fixture.
This is the single most common capital misallocation in additive manufacturing operations, and it is invisible on the shop floor because the printing station is the loud, expensive, visible one. The constraint is almost always somewhere quieter.
The line ships 352 parts because finishing is the ceiling, and the small gap between 355 and 352 is normal process loss. The honest answer to “why is output flat” is that the twelfth machine spent its capital raising an already-sufficient capacity by nine percent while the actual constraint was never touched.
Finding the Constraint Without Guessing
Constraint identification is a measurement exercise, not a judgement call. It takes four half-days of observation and produces a number for each station: how many parts per shift can pass through, counting only time when the station is genuinely capable of accepting work.
The measurement rules matter more than the arithmetic.
- Count parts passing the station, not parts arriving. A station with 40 parts waiting and 20 processed in a shift has a capacity of 20, regardless of what the schedule asked for.
- Exclude starved time. If finishing sat idle because printing had not delivered yet, that hour is not capacity. Count only hours where work was available and the station was still the limiter.
- Include the operator, not just the equipment. A blast cabinet that runs at 90 parts a shift when attended continuously runs at 55 when the same operator also handles support removal on a second bench.
- Repeat across shifts. A constraint that only appears on the night shift is a staffing constraint, and the fix is a different one entirely.
What you're looking for: More than about half a day of banked work means the queue is real and the finishing bench is the constraint. Almost no banked work means printing really is the limiter, and an equipment conversation is justified.
Takt Time: Sizing the Line to the Order Book
Takt time is the pace the line must hit to satisfy demand. It is demand divided by available working time, and it is the reference point against which every station's capacity is compared. Without it, a line is either overbuilt or permanently late, and nobody can tell which.
A bureau quoting a 5-day standard lead time on a 2-shift pattern has about 80 productive hours a week. If the order book is 400 parts a week, takt time is 12 minutes per part. Any station slower than one part per 12 minutes is a constraint.
The table explains why shift structure is a capacity lever that costs nothing but wage hours. Moving a 400-part order book from a single day shift to three shifts raises takt time from 8.4 to 18.0 minutes per part — more than double the pace allowance — without buying a single machine. A line that looks capacity-constrained on one shift is often comfortably capable across three.
The distributor angle here is direct. A customer who understands takt time buys machines against a measured gap rather than a feeling, and a gap measured in minutes per part is a far more persuasive starting point than a rough impression that things are busy.
Balancing the Line: Four Levers, In Order
Once the constraint is known, the work of balancing is straightforward. The rule is to raise the constraint's capacity before adding capacity anywhere else, and to prefer the cheapest lever that closes the gap.
- Move work off the constraint. If finishing is the bottleneck because operators also remove supports, splitting support removal into its own station and its own operator can lift finishing capacity by 20–30% with no capital at all.
- Reduce the constraint's work content. Part design determines finishing labour. A printed fixture that comes off the plate with a flat base needs a fraction of the sanding that a part printed at an angle with dense supports does. This is where build orientation stops being a print-quality decision and becomes a capacity decision.
- Add capacity at the constraint only. A second blast cabinet at the finishing bench costs a fraction of a printer and lifts the line's output directly, because the constraint is the only station where added capacity converts into shipped parts.
- Buffer deliberately. A small, bounded queue in front of the constraint protects it from starving. An unbounded queue in front of it just hides defects in a growing pile of unfinished work.
Levers one and two are free. Levers three and four cost money. Operations that work them in order routinely lift output 15–25% before spending anything, and they spend far more accurately when they finally do.
Work In Progress Is the Tell
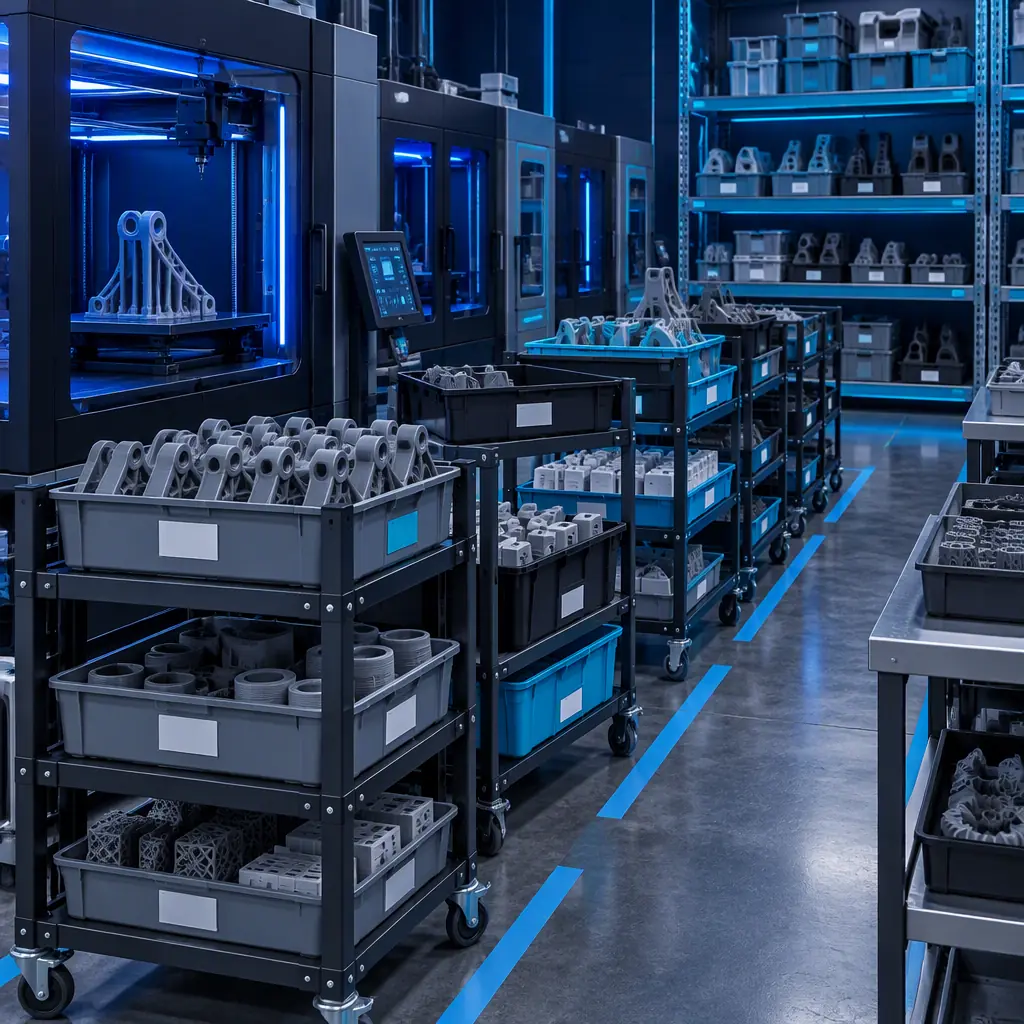
Work in progress is the most diagnostic number on the floor because it accumulates exactly in front of the constraint. A tally of unfinished parts by station, taken at the same time each day for a week, draws a profile of the line that no schedule can hide.
The second row is the one distributors need to hear clearly, and it is the one customers least want to accept. A stable WIP profile with idle printers means the operation has spare capacity it cannot sell. The fix is commercial, and selling that customer another machine makes their position worse.
The measurement and inspection angle deserves a note because it is a constraint that looks like a quality problem. When parts queue at inspection, the usual reaction is to add inspection labour. The better first move is to check whether the sampling plan is tighter than the application requires — a fixture that holds ±0.5 mm does not need every unit measured to ±0.05 mm, and the methods for setting a proportionate plan are covered in our part metrology guide.
Scheduling Rules That Keep a Balanced Line Balanced
A balanced line degrades quickly under the wrong scheduling habits, because every station optimises for its own local efficiency unless something stops it. Three rules hold the balance in place.
- Release work at the constraint's pace. Starting every job the moment a printer frees up floods the finishing bench. Release orders so that the finishing bench sees a steady flow rather than a wave.
- Never let the constraint wait for a decision. A missing material choice or an unapproved drawing stalls the one station that sets output. Keep approvals ahead of the constraint by at least a day.
- Measure the line, not the machine. Machine utilisation is an input metric. Parts shipped per week is the output metric, and it is the only one that reflects whether balancing is working.
These rules connect directly to how orders are priced, because a schedule that protects the constraint changes what a rush job actually costs. A rush order does not just consume machine time — it displaces the sequence at the finishing bench, which is why the rush premium mechanics described in our service bureau economics guide belong in any balanced line's quoting method.
What you're looking for: A ratio that drifts above roughly 1.1 and stays there means WIP is accumulating and a constraint is being starved or overloaded. A stable ratio near 1.0 across weeks is the signature of a balanced line.
Applying This to a Print Farm Upgrade Decision
For a distributor, constraint analysis is the tool that converts a vague enquiry into a specific, defensible order. The customer who says “we need more capacity” and the customer who says “finishing caps us at 355 parts and our takt time is 12 minutes” will buy very different things, and only the second conversation reliably produces a repeat relationship rather than a returned machine.
The same reasoning scales to larger operations. Where a farm runs many machines across shifts, the constraint shifts with the shift pattern and the product mix, which is why the throughput economics of running multiple print cells together are covered separately in our IDEX print farm economics guide. For operations still establishing their first measured baseline, the scheduling framework in our print farm operations guide and the formats discussion in our medium-format floor guide both start from the same premise: measure the stations before changing the equipment.
Precise3D on Measured Capacity
At Precise3D, the capacity conversation with a customer starts with the numbers on their floor, because a printer sold against a constraint it cannot relieve is a printer that returns to us. Our Pro X1 and OpenSource1 platforms pair a 320°C hotend with an actively controlled heated chamber and a rigid frame designed to hold dimensional consistency across long unattended runs — the reliability characteristics that determine whether a print station can actually deliver the capacity its nameplate suggests.
Every unit ships with CE LVD (EN 62368-1:2014+A11:2017) and RoHS (EU 2015/863) documentation, and our 3,500 sqm Shenzhen production network applies a documented control plan at incoming and outgoing QC. For distributors, we supply the fleet-level documentation — spares lists, sensor and consumable mappings, and maintenance intervals — that keeps a measured line running at its measured capacity rather than drifting back to guesswork.
Reviewed by the Precise3D production engineering team. Station capacities, takt times and WIP thresholds described here are illustrative ranges provided for guidance and are not a guarantee of performance for any particular operation. Measure your own stations before acting on capacity figures.
Balancing a Production Line?
Want the Station Capacity Worksheet for a Print Farm?
Tell us how many machines you run and where parts pile up. We will send a station-by-station capacity worksheet, the takt-time table for your shift pattern, and the machine specification that matches the constraint you actually have — not the one that is easiest to sell.