
Live Z Offset and First-Layer Tuning — A Measurable Calibration Loop
How to tune 3D printer first-layer Z offset as a measurement loop: probe versus manual reference, layer-thickness targets, and the correction maths for field service.
Print Farm Job Scheduling and Queue Software — Rules Before Tools
Print farm scheduling explained as four operating rules then three software tiers, with WIP limits, lead-time quoting from backlog, and fleet integration requirements.
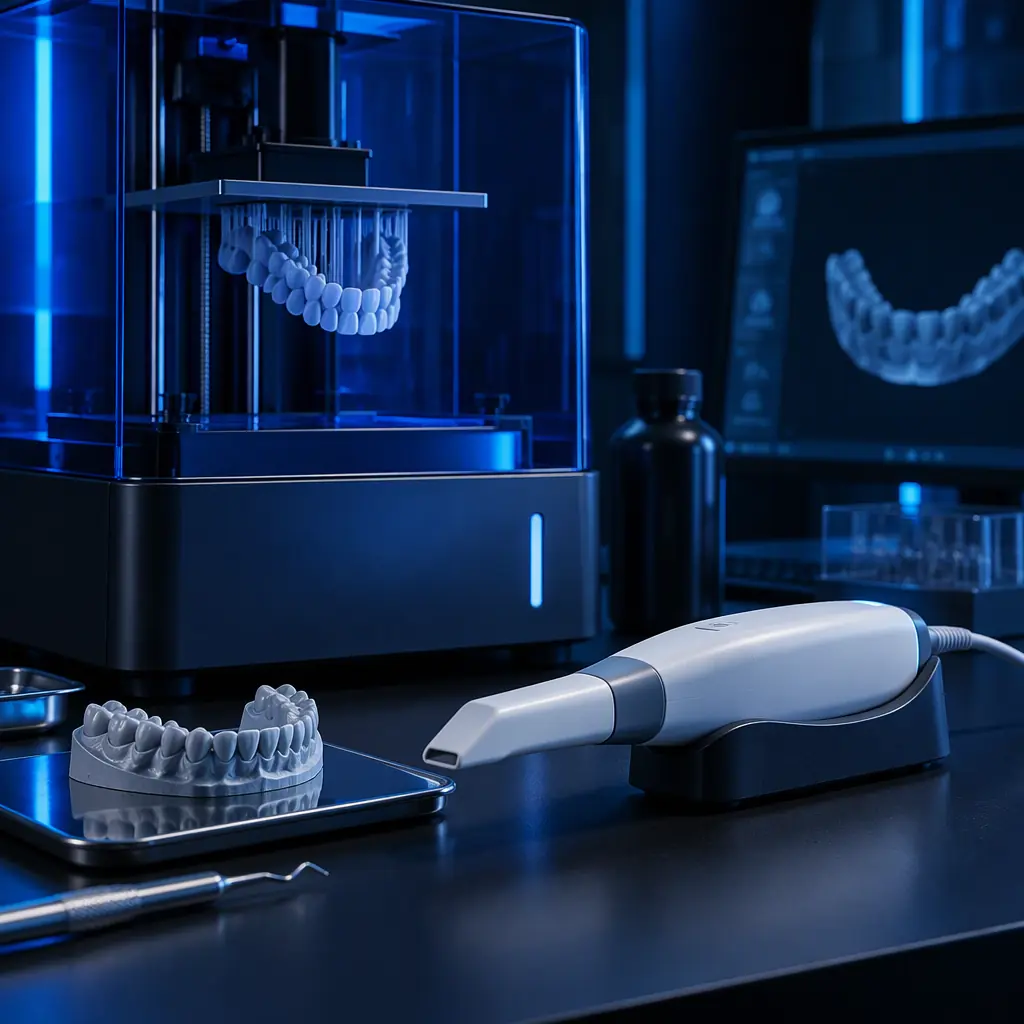
From Intraoral Scan to Printed Model — Closing the Dental Digital Loop
How to match an intraoral scanner to a 3D printer: scan accuracy thresholds, STL handoff, model and aligner printing, resin selection, and the file-flow errors that break a closed dental workflow.
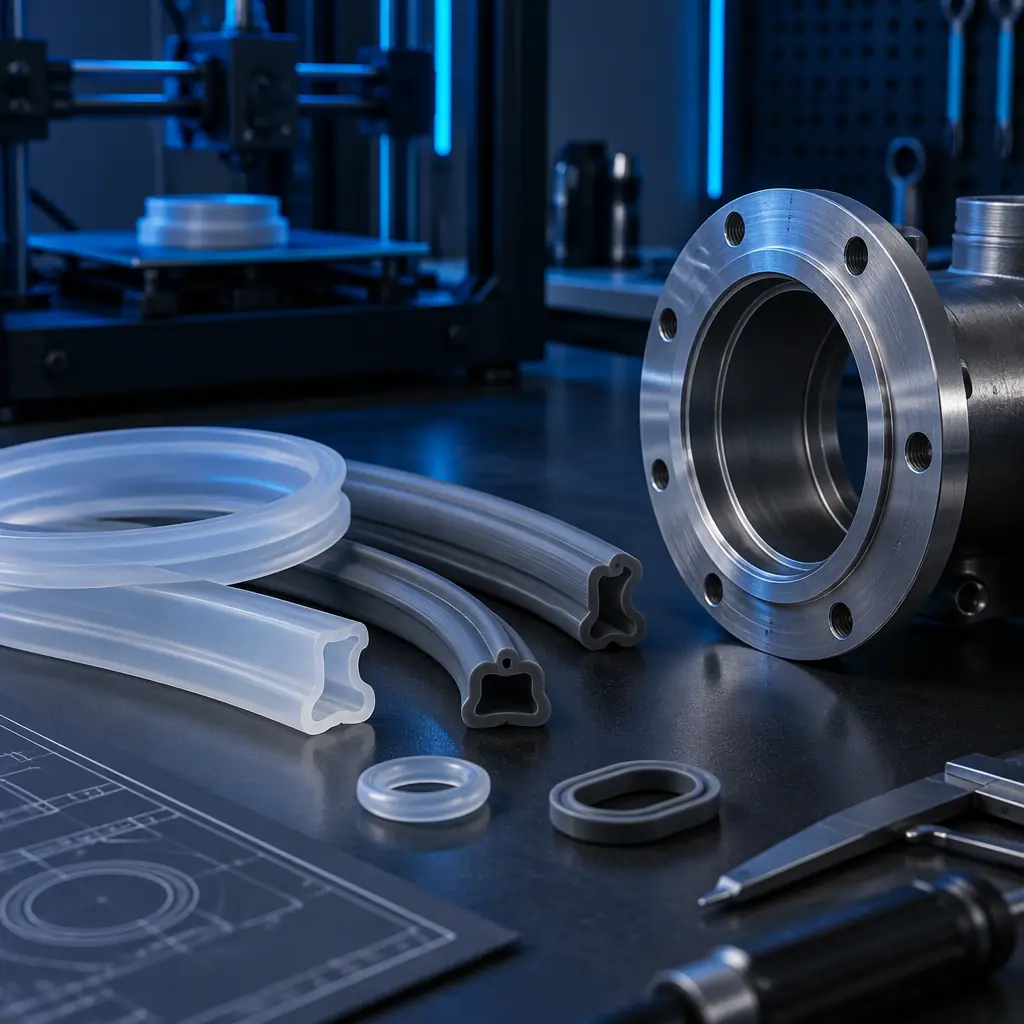
Silicone Seals and Gaskets — LSR, TPU and Cast-in-Printed-Mould Routes
How to print silicone seals and gaskets: liquid silicone rubber versus TPU versus printed moulds for cast silicone, with material data, compression set and the sealing geometry that works.
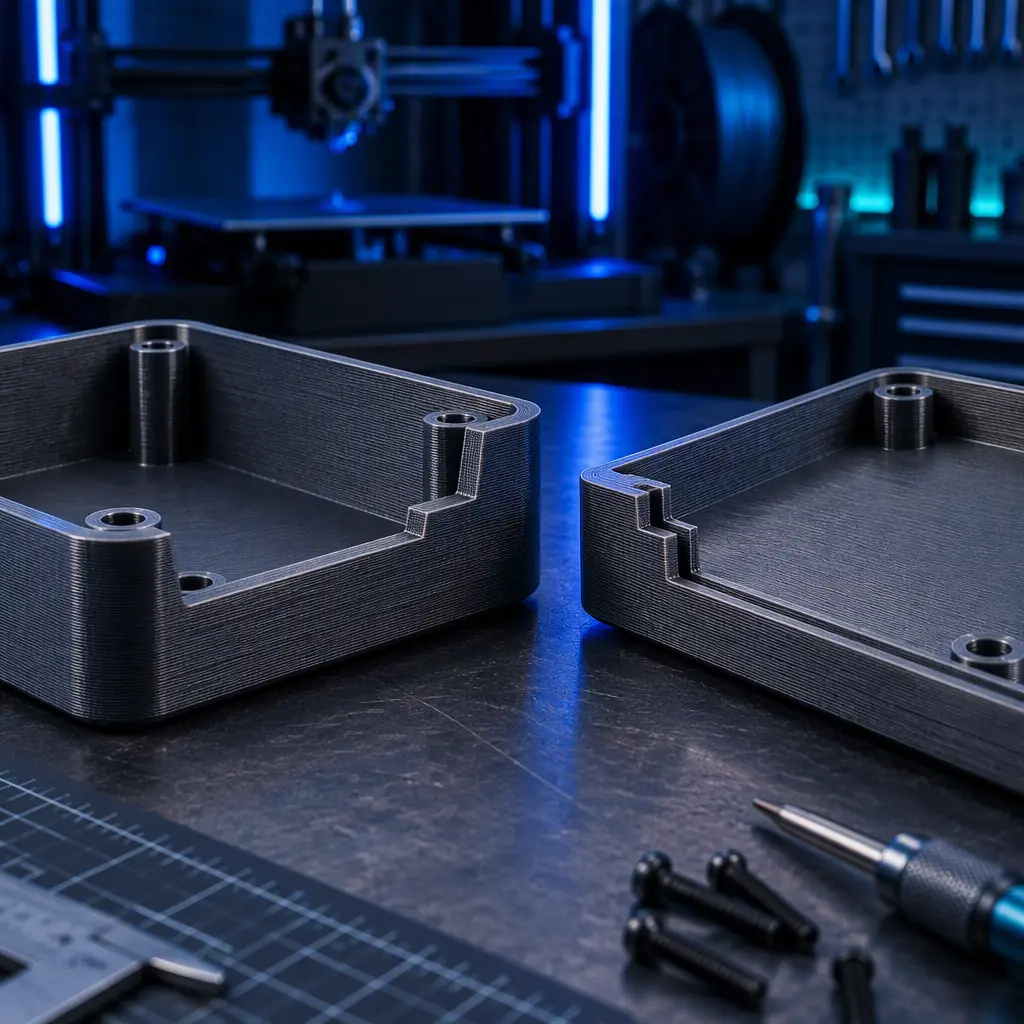
Joining 3D Printed Parts — Ultrasonic, Hot Plate and Laser Welding Compared
Which plastic welding method suits 3D printed assemblies: ultrasonic, hot plate, laser and solvent bonding compared by material, joint geometry, cycle time and tooling cost.
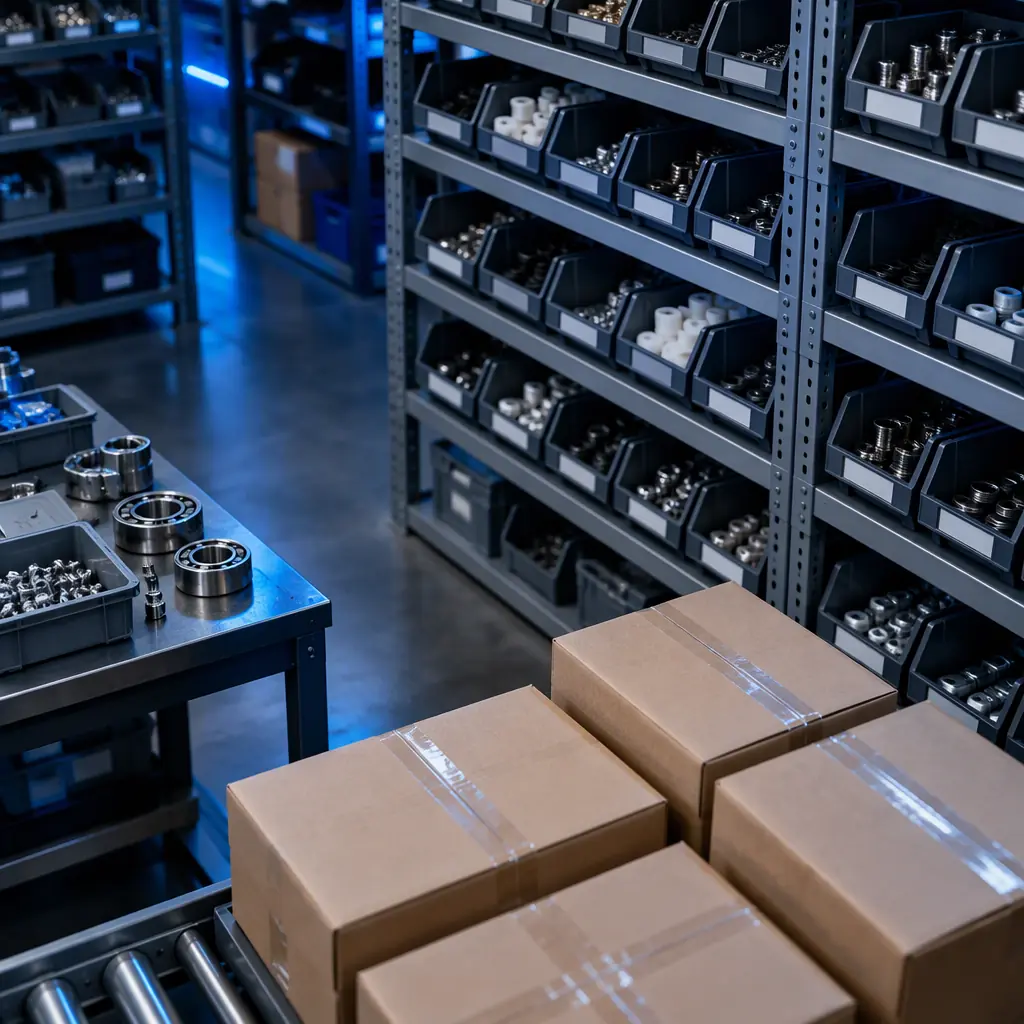
Thirty Printers Across Five Sites — the Parts Logistics That Keeps Them Running
A three-tier parts model for multi-site 3D printer fleets: on-site consumable buffers, regional forward stock for hotend kits, and a central depot for boards and motors.
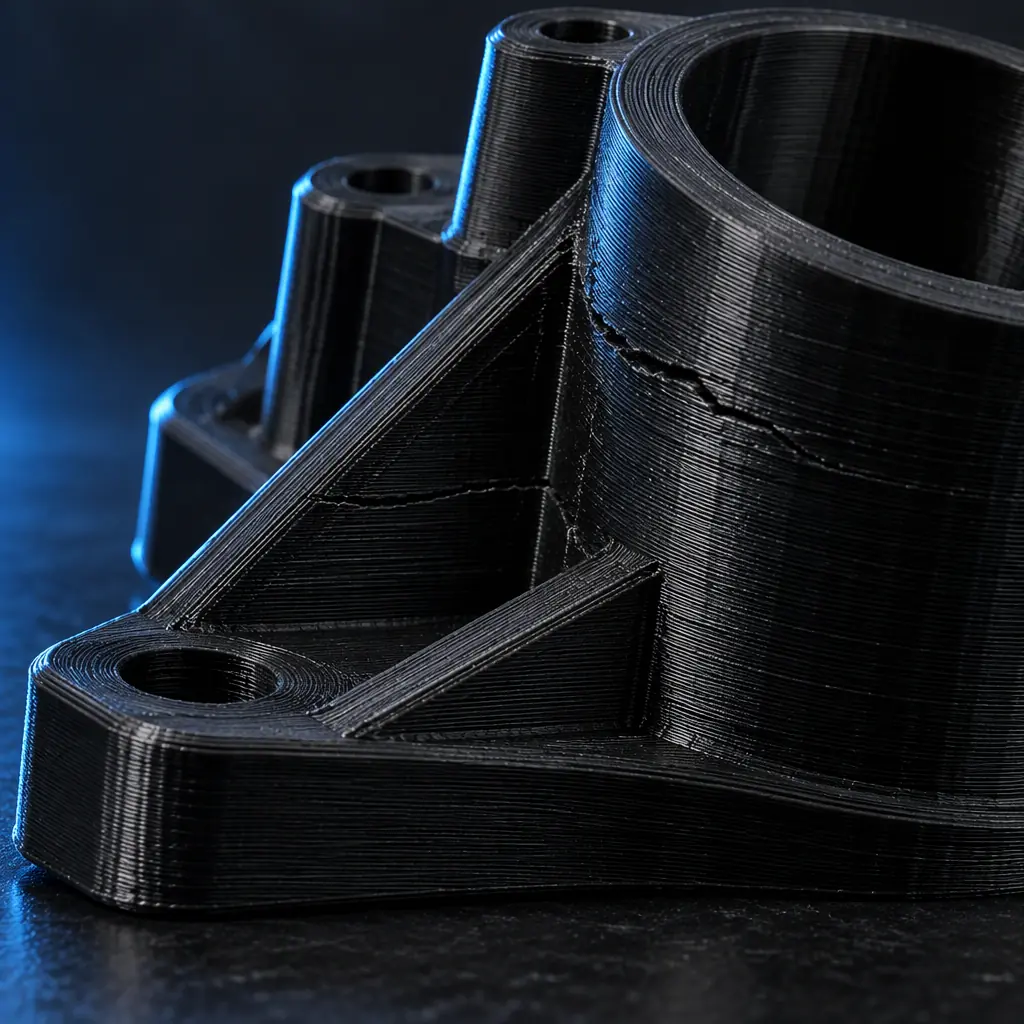
A Heated Chamber Is a Yield Investment, Not an Energy Cost — Here Is the Arithmetic
Size a heated chamber at 15-25 W per litre for 60 C and 30-40 W per litre for 100 C, then build the ROI case from the customer's own tall-part failure rate.
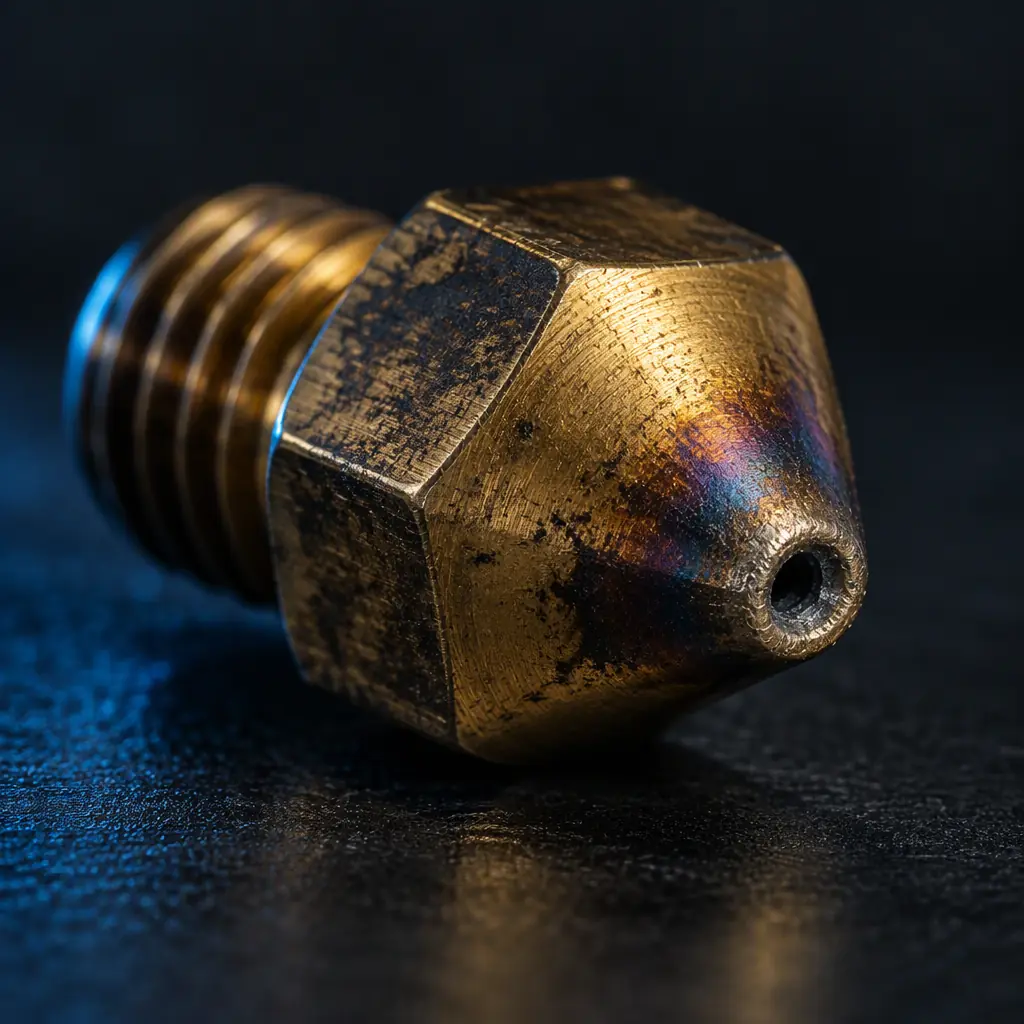
Hotend Failures Escalate in a Fixed Order — Here Is the Ladder, and the Part Number at Each Stage
Hotend failures escalate in a fixed order: nozzle wear, heat creep, heater cartridge and thermistor drift, then full assembly replacement. Diagnose by stage and quote the right part first time.
Engineering Design for 3D Printing, Five Decisions in the Right Order
Datum first, orientation on the drawing, tolerance by process: a five-step engineering design workflow for 3D printing that survives a second source.
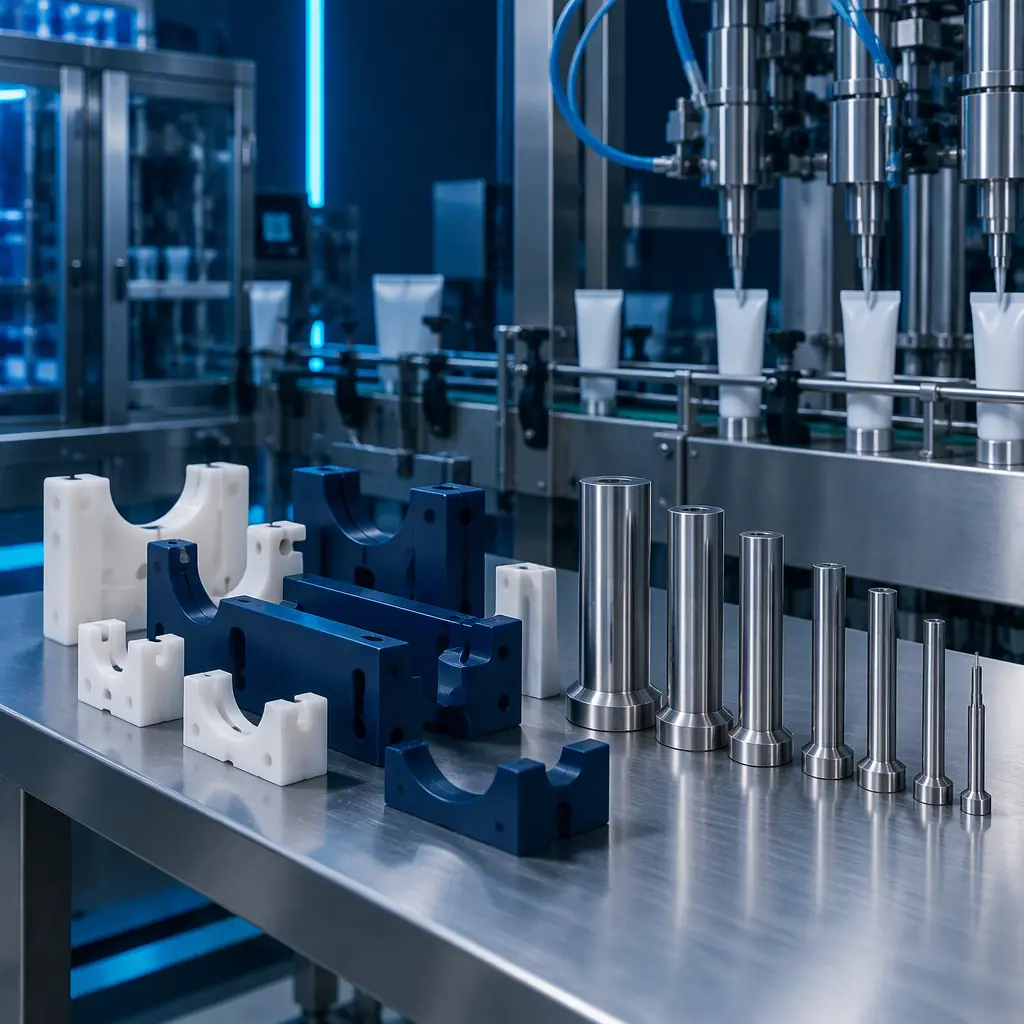
3D Printing for Cosmetic Tube Packaging Tooling and Change Parts
Cap inserts, decoration pads, filling change parts and fixtures: where additive tooling pays on a cosmetic tube line, and how material is chosen.
