What a Print Farm Actually Is, and When It Stops Being a Farm
A print farm is a production cell built from many identical machines rather than one large one. The logic is straightforward: if a part occupies 300 cubic centimetres, four machines that each build 400 cubic centimetres produce four times the throughput of one machine building 400 cubic centimetres, and they do it with four independent job queues. The farm model wins on throughput per dollar and loses on labour per machine, and everything that goes wrong in a farm traces back to that trade.
The break point is not a machine count, it is a labour ratio. Below roughly eight machines, one operator can reasonably load, unload, inspect and restock every machine on a shift, and the farm behaves like a single machine with a bigger bed. Above twelve to fifteen machines, a single operator cannot keep every machine fed, and the farm either needs a second operator or it runs at reduced uptime. That threshold, not the capital budget, is what determines whether adding machine nineteen is profitable.
This matters because the common failure mode in farm planning is buying machines on throughput and then discovering the constraint was operator attention. A farm of twenty machines with one operator typically runs at 55 to 70 percent effective uptime. The same machines with two operators and a job-staging discipline run at 80 to 90 percent. The machines did not change, the arithmetic did.
For a buyer deciding between fleet architecture and a single large-format machine, that labour question is the decision. Our guide to large-format industrial machines covers the single-machine route, and this article covers the fleet route.
The Four Numbers That Decide Farm Profitability
Farm economics reduces to four measurable quantities. Every other input, from resin cost to electricity, is either small enough to ignore or is a consequence of these four.
Effective uptime is the master number and it is the one most often estimated optimistically. A machine that is physically capable of 7,000 hours a year does not deliver 7,000 hours of paid work. It delivers job hours, and job hours are lost to four things: the gap between one job finishing and the next starting, failed prints that consumed machine time, maintenance windows, and idle time when no order is queued.
Chamber utilisation is the second number and it is a scheduling problem, not a hardware problem. Filling a chamber with one large part and three small parts that nest alongside it raises utilisation without any capital cost. Farms that quote per-part prices without checking chamber utilisation are effectively subsidising their customers' spare volume, and that is why identical machines in different shops produce per-part costs that differ by a factor of two.
Failure rate deserves attention because it compounds. At 1.5 unplanned failures per machine per month across 20 machines, that is 30 incidents a month, which is roughly one per working day. Each incident consumes machine time, material, and operator attention at the exact moment the operator was supposed to be starting the next job. This is the mechanism by which a farm's uptime collapses non-linearly as machine count grows: incidents scale linearly, but operator attention does not.
Cost Per Part on a Farm, Built From Line Items
The honest way to price farm output is to build the hourly rate first and then divide by parts per hour. Most farm quotes skip the first step, which makes them impossible to audit. Here is the decomposition for a mid-size farm machine running engineering filament.
Note which line is largest. On a farm, allocated labour typically exceeds depreciation, and on a single-machine shop the reverse is true. That inversion is the whole economic character of a farm: it is a labour-constrained business wearing a capital-equipment costume. It also explains why a farm that raises uptime from 60 to 85 percent improves unit cost by roughly 30 percent without buying anything.
Material cost is deliberately absent from the table because it scales with the part, not the machine. For a part consuming 120 grams of engineering filament at $32 per kilogram, material is $3.84, plus support removal and any failed-print allowance. A realistic failure allowance is 3 to 8 percent of material on a well-run farm and 12 to 20 percent on a farm with inconsistent profiles.
The per-part cost then falls out of cycle time. A part with a 6-hour build and 40 percent chamber utilisation produces, in effect, 2.4 paid machine-hours per 6 clock hours when the chamber is shared. At the $2.40 mid-range rate that is $5.76 of machine cost plus $3.84 of material, or $9.60 per part at that utilisation. Halving the cycle through profile tuning, or doubling the nesting density, halves that machine component. Our guide to cost per part and unit economics walks the same arithmetic for a single machine, and our overview of filament quality evaluation covers the material-side variables that drive the failure allowance.
Why Uptime Beats Machine Count Every Time
Buying a twenty-first machine adds 5 percent throughput at the same uptime. Raising uptime from 65 to 85 percent adds 31 percent throughput across every machine already owned. The second option is almost always cheaper, and it is the one farms skip because it does not come with a delivery date.
The uptime levers, in the order they usually pay back:
- Job staging. A gated queue in which the next job is sliced, checked and staged before the current one finishes removes most of the transfer gap. Realistic gain: 5 to 12 percentage points.
- First-layer reliability. A significant share of failed prints die in the first ten minutes. Automated bed levelling plus a documented first-layer inspection step cuts that class of failure substantially. Realistic gain: 4 to 9 points.
- Predictive maintenance on wear items. Nozzles, belts, and bearings are consumables with knowable lives. Replacing them on a schedule rather than on failure converts unplanned downtime into planned downtime. Realistic gain: 3 to 7 points.
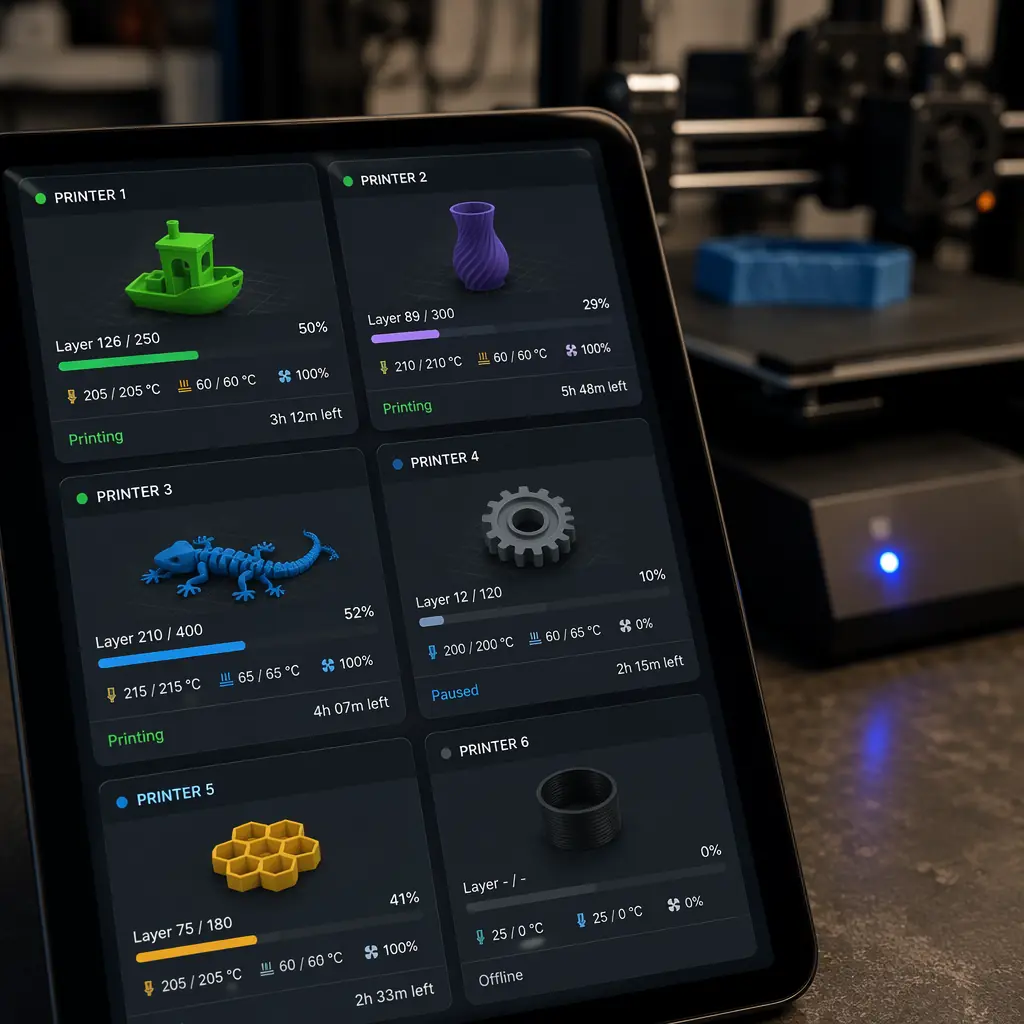
- Remote monitoring. Cameras and failure detection let one operator watch more machines at once, which directly raises the machines-per-head ceiling. Realistic gain: shifts the ceiling, not the rate. See our guide to AI print monitoring and failure detection for what detection actually catches.
Notice that three of those four levers are procedural, not hardware. That is the recurring finding in farm operations: the constraint is the routine, and a farm that buys machines instead of routines simply scales its existing inefficiency.
Scheduling: Where Farms Lose Money Quietly
A farm's job queue is a scheduling problem with a specific pathology: the jobs that are easiest to start are not the jobs that are most profitable to run, and in an unmanaged queue the easy jobs win. Three scheduling disciplines prevent that.
Nest by material, not by due date
Material changes cost time: purging, temperature transitions, and the risk of contamination in the hot end. Grouping jobs by material and accepting a slightly later due date for a lower-priority job usually beats running materials in strict date order. The exception is a genuinely urgent job, which should be priced to reflect the purge cost it imposes rather than absorbing it silently.
Quote a minimum chamber fill
A farm that accepts single small parts as standalone jobs is selling machine hours at a chamber utilisation of 8 percent. Either the price reflects that or the job waits to be nested. The clean policy is a stated minimum billable machine time, which converts a loss-making job into a neutral one and pushes the customer toward batching their own orders.
Keep one machine off the queue
Reserving one machine for urgent work, engineering trials and sample prints looks like an 5 percent capacity sacrifice. In practice it protects the schedule from being entirely rewritten by a single rush order, which is worth more than the capacity. Farms that run every machine on the production queue have no slack, and no slack means every disruption propagates to customers.
Failure analysis at the farm level deserves its own discipline. When a print fails, the record should capture machine, material lot, profile revision, failure mode and elapsed time. Twenty machines generating failures without a shared record produces a farm that cannot tell whether its failure rate is a hardware problem, a material problem or a profile problem. Our guide to cost of poor quality and 8D root cause analysis explains how to structure that record so it converges on a cause instead of accumulating anecdotes.
What you're looking for: If the answer is a machine specification rather than a logged figure, the farm is not measuring the number its pricing depends on. A supplier who can show job hours delivered against calendar hours available is running a managed operation; one who quotes theoretical capacity is quoting a brochure.
Fleet Composition: Identical Machines or a Mixed Floor
There is a real argument for a mixed floor. A farm of twenty identical machines can only accept jobs that fit that build volume and that material set, so a mixed floor broadens the order book. The counter-argument is that every distinct machine type multiplies spare parts inventory, profile libraries, operator training and maintenance procedures.
A workable compromise that many farms converge on:
Keeping the bulk on one platform means one spare parts kit, one profile set and one maintenance routine cover most of the floor. Our guide to critical spares kit design covers what that stocking list should contain, and the discipline matters more on a farm than in a single-machine shop because an unplanned stop is multiplied by the number of machines sharing the consumable.
Power and environment set the practical ceiling on density. Twenty enclosed printers drawing an average of 450 watts each is 9 kilowatts of continuous load, plus HVAC to remove the heat they release into the room. A farm floor that ignores this ends up with machines in a room that drifts several degrees warmer than the enclosure setpoints assume, which shows up as inconsistent results rather than as an obvious failure. Our guide to power supply selection covers the per-machine side of that calculation.
Building the Business Case for Machine Number Twenty-One
The marginal machine test is simple, and running it explicitly is what separates a planned farm from a growing pile of equipment.
Take the loaded machine rate derived above, apply your measured effective uptime, and multiply by the billable hours the new machine can actually fill. If your order book has more queued hours than your current fleet can deliver at target lead time, the new machine fills immediately and the case is straightforward. If your order book does not, the new machine reduces the utilisation of every existing machine, and the marginal case is negative even though the absolute throughput rises.
That is the arithmetic farms get backwards. Machine count is an output of demand, not an input to it. A farm that adds capacity ahead of a queue ends up with lower utilisation, higher allocated overhead per part, and a pricing problem it cannot solve by working harder.
The other half of the case is lead time. A farm running at 95 percent utilisation quotes long lead times, and long lead times lose the orders that would have filled the capacity. There is a defensible strategy of holding utilisation near 80 percent deliberately, quoting short lead times, and winning the orders that competitors cannot take. That strategy is invisible on a capacity spreadsheet and very visible on a profit and loss statement.
If you are planning farm capacity and want the arithmetic checked against realistic machine performance rather than brochure figures, send us your part mix, target monthly volume and shift pattern. We build engineering-grade machines intended for exactly this kind of continuous production duty, and we would rather help you size the fleet correctly than sell you machine twenty-one.